Getting Started with 3MS
This page walks through the first menuconfig pass for a 3MS MMU — the
screens you'll see, in the order you'll see them, and the handful of choices worth
pausing on. It's the first of a set of getting-started pages; other pages cover
toolhead calibration and multi-unit setups in more depth. Here we're just getting
a 3MS installed and talking to Klipper.
Menuconfig Installer
From your Happy-Hare checkout:
./install.sh
The very first time you run this, there's no .mmu_config yet, so the installer
drops you straight into menuconfig — no separate flag needed.
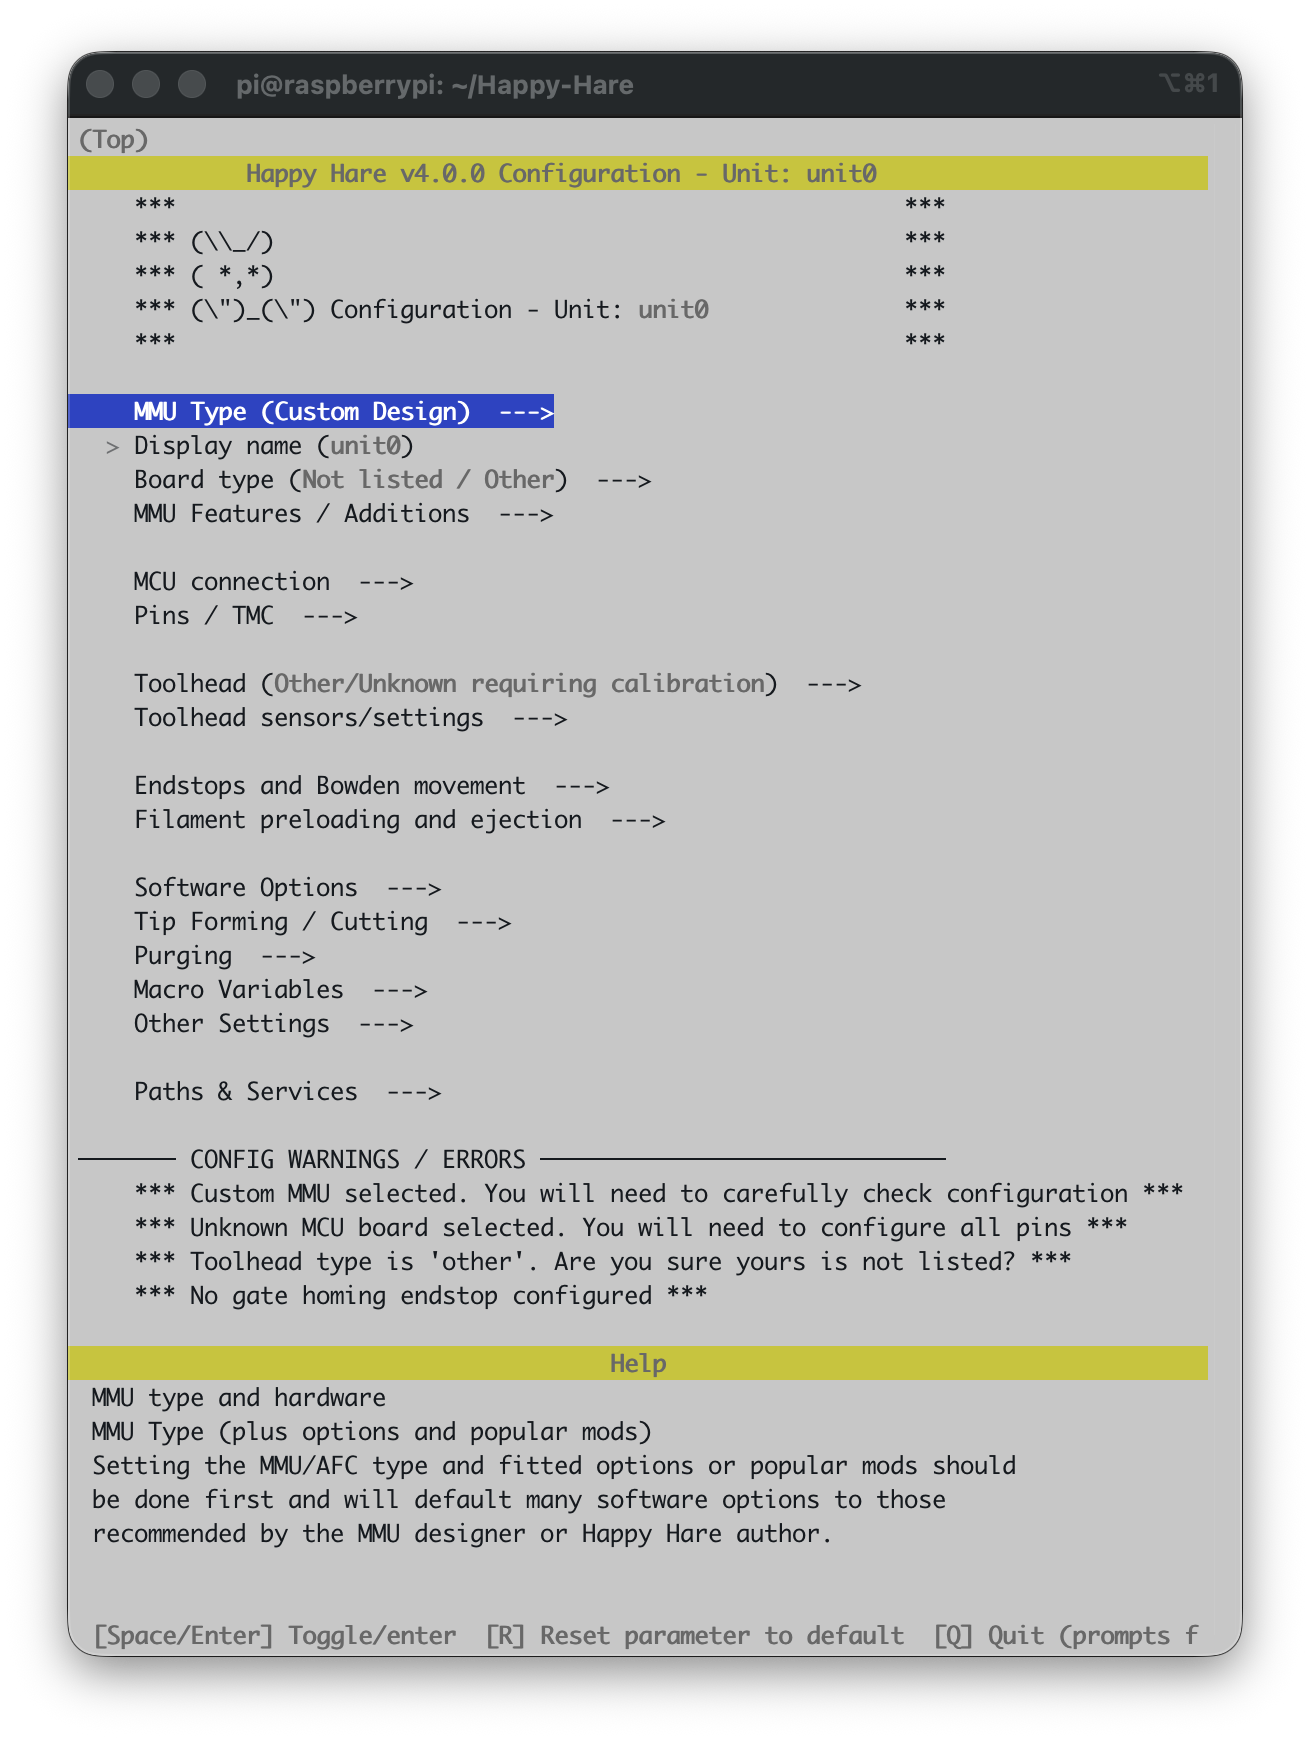
This is the installer's default state: MMU Type is Custom Design, the board is
unknown, and the CONFIG WARNINGS / ERRORS panel at the bottom lists exactly
that — four things still need a decision. As soon as you pick a real MMU type,
most of these clear themselves.
A quick word on the controls, since you'll use them constantly:
- Arrow keys move the highlight; Enter (or Space) opens a submenu or toggles/selects the highlighted item.
- Esc or Left Arrow key backs out one level; from the top level it offers to save.
- R resets the highlighted parameter back to its default — useful any time you've typed something and want to back out cleanly without hunting for the original value.
Choosing the MMU type
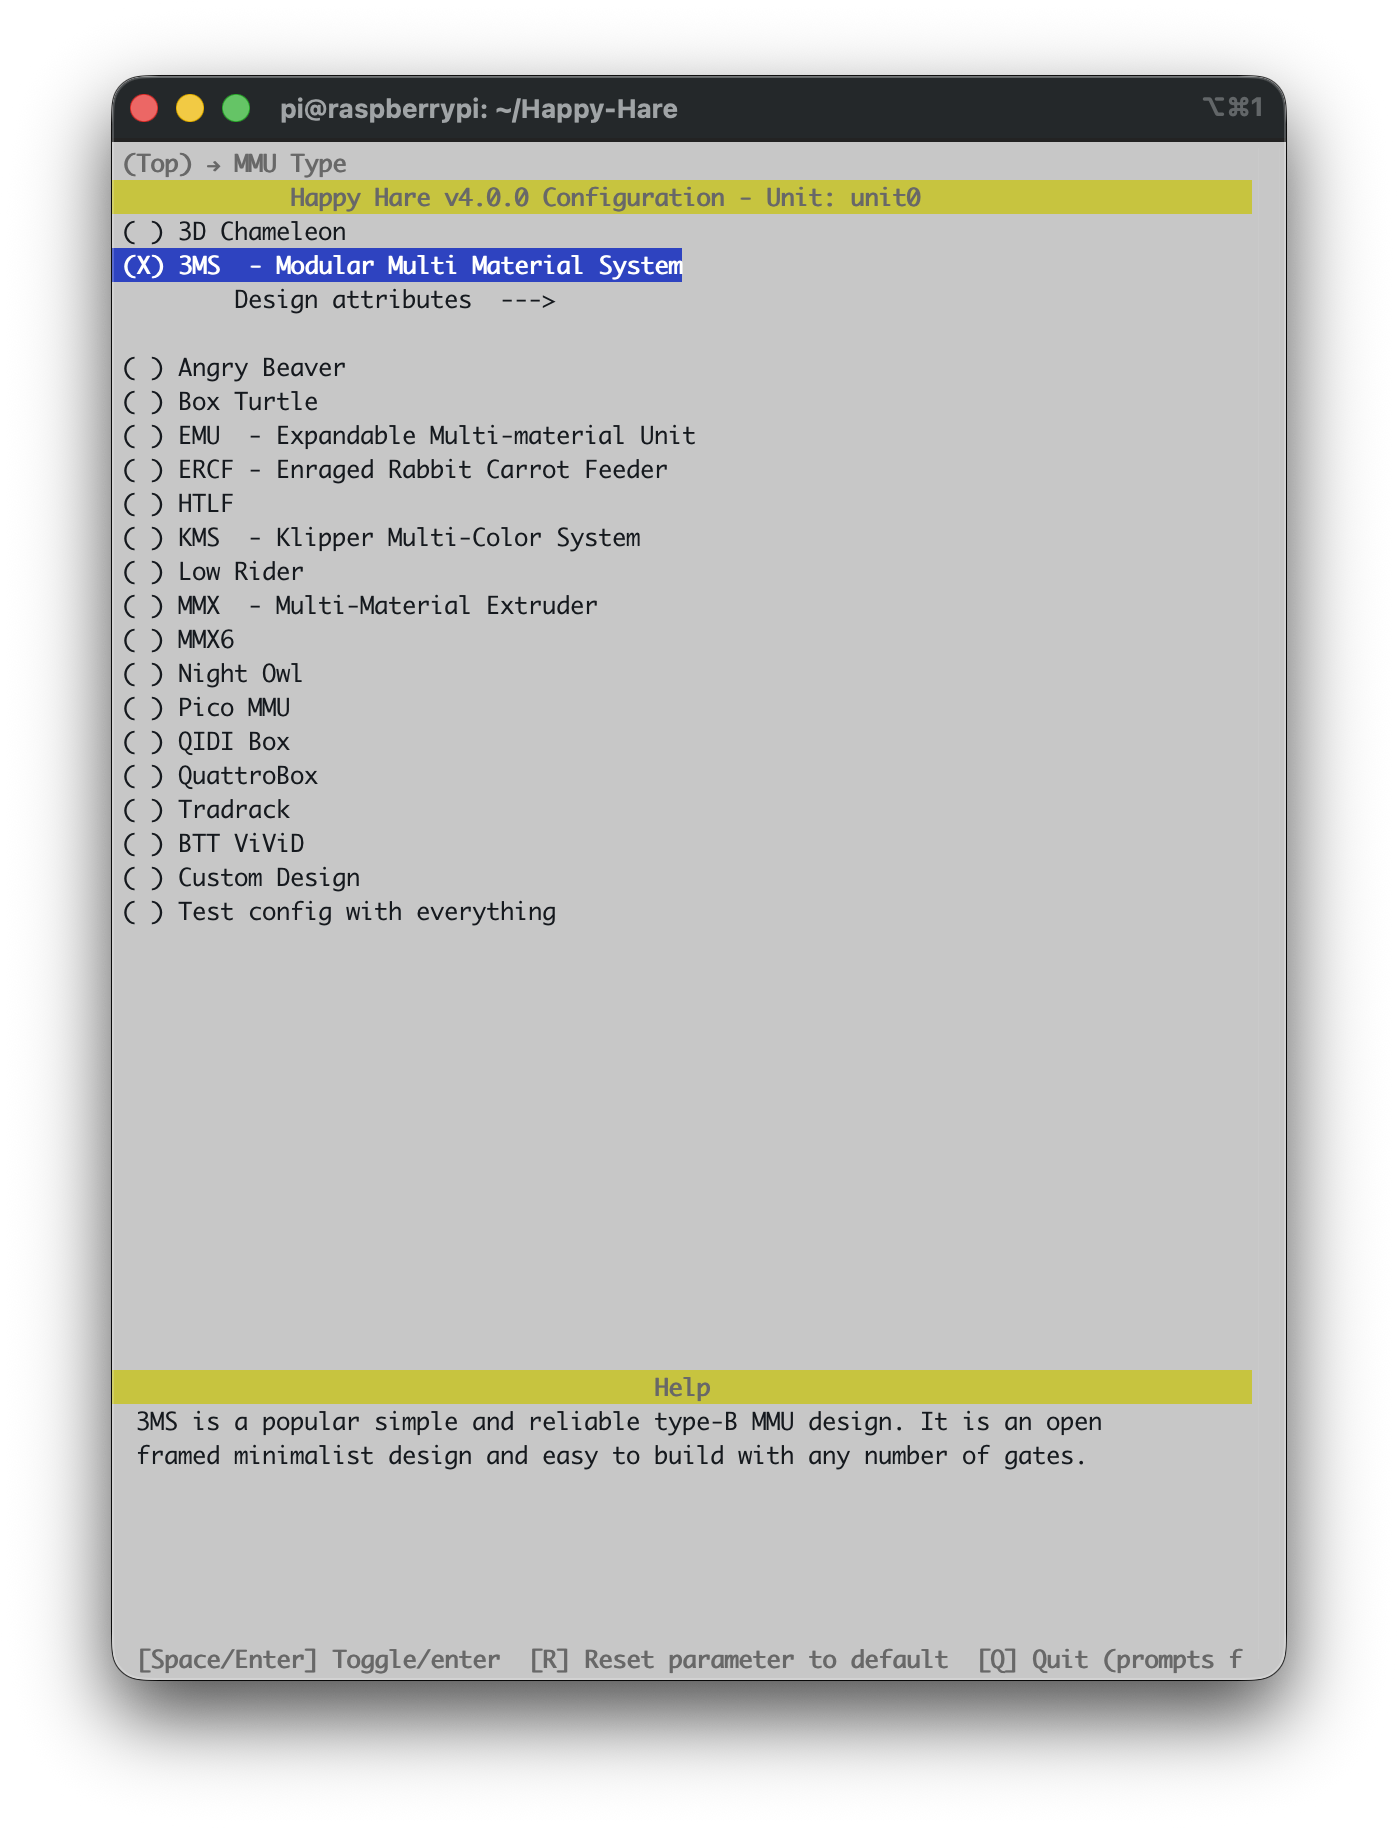
Highlight MMU Type and press Enter. Use the arrow keys to navigate up to 3MS and press Space to select it:
Use the left arrow key to go back to the main screen:
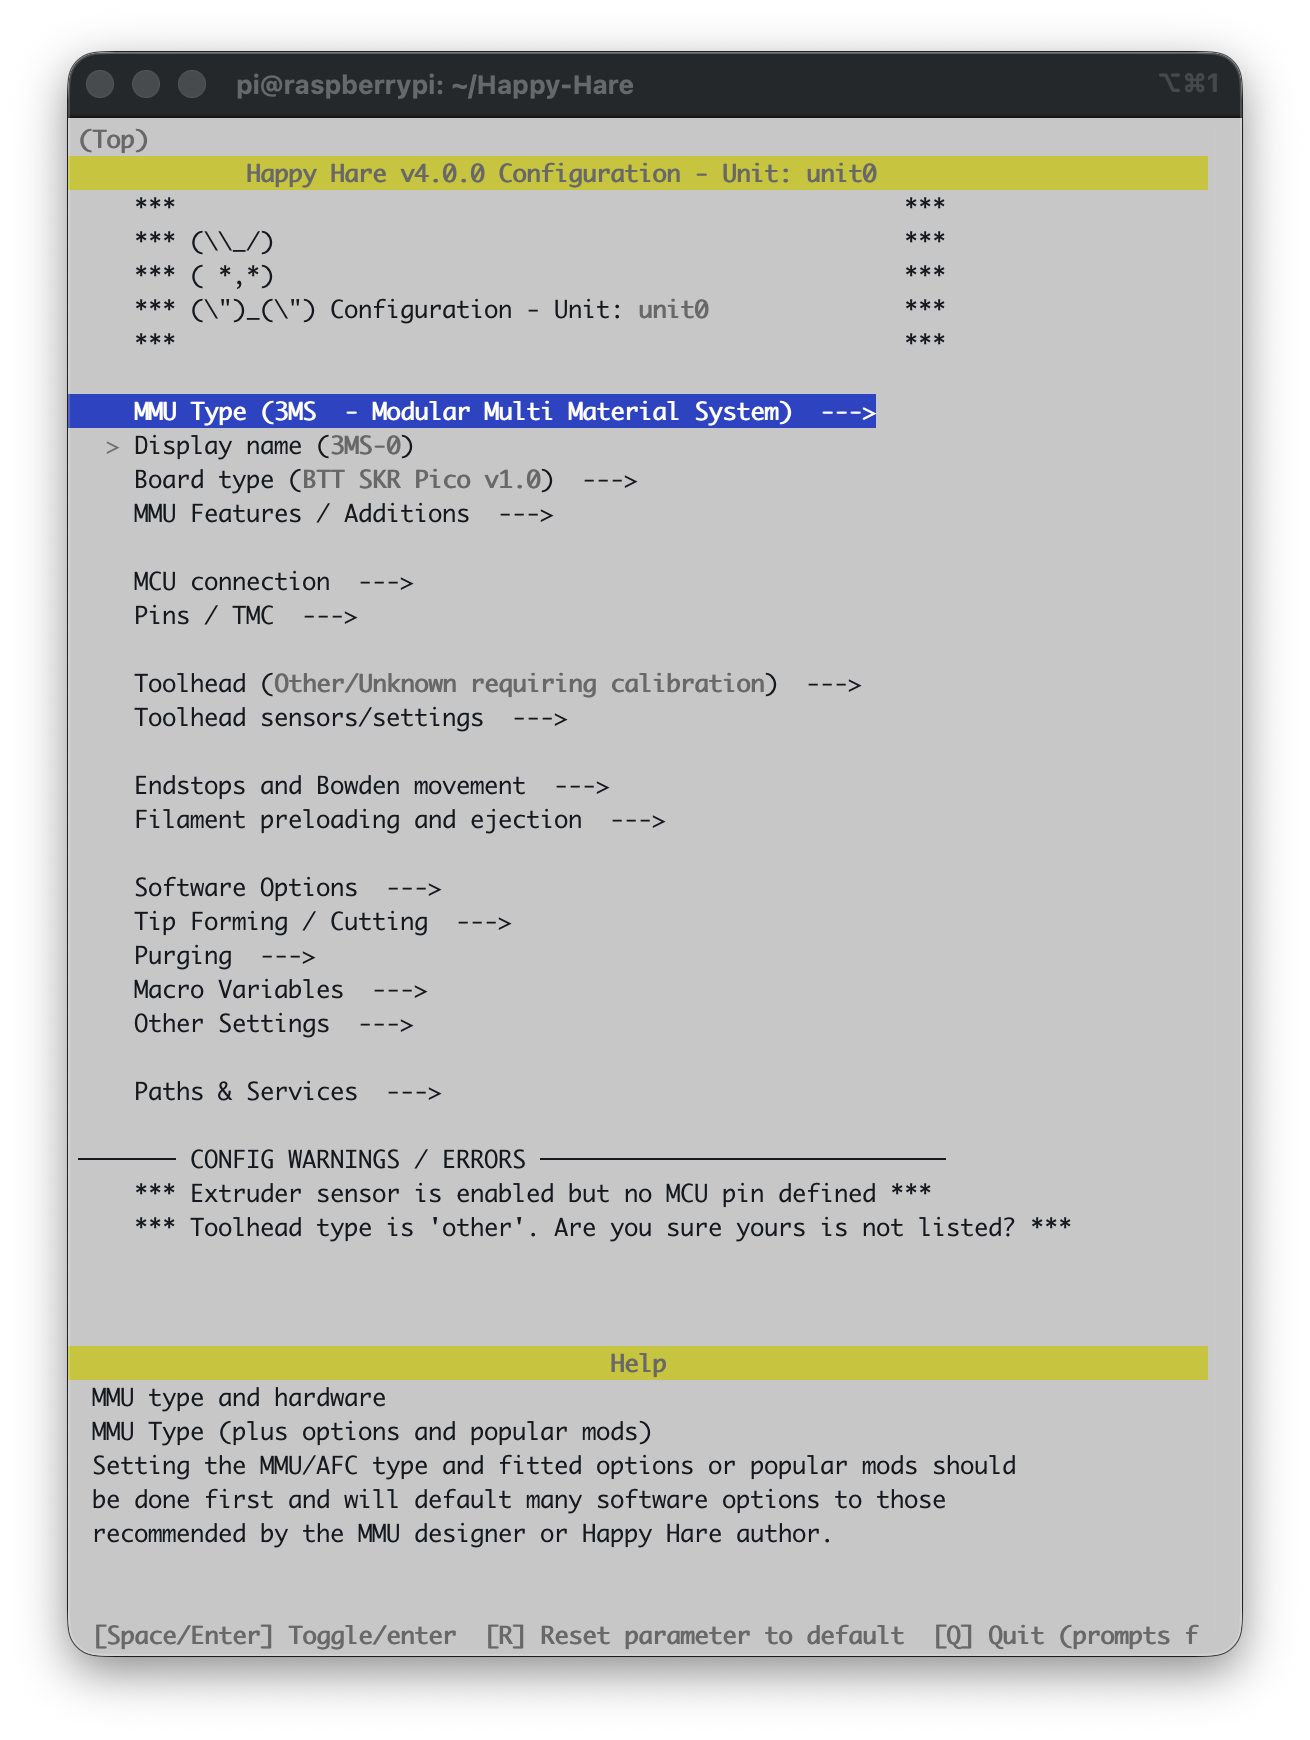
If you scroll to the bottom, you'll notice two warnings because Happy Hare still doesn't know your toolhead, and that's covered in a different getting-started page. Don't worry about it here.
Board type
Enter Board type:
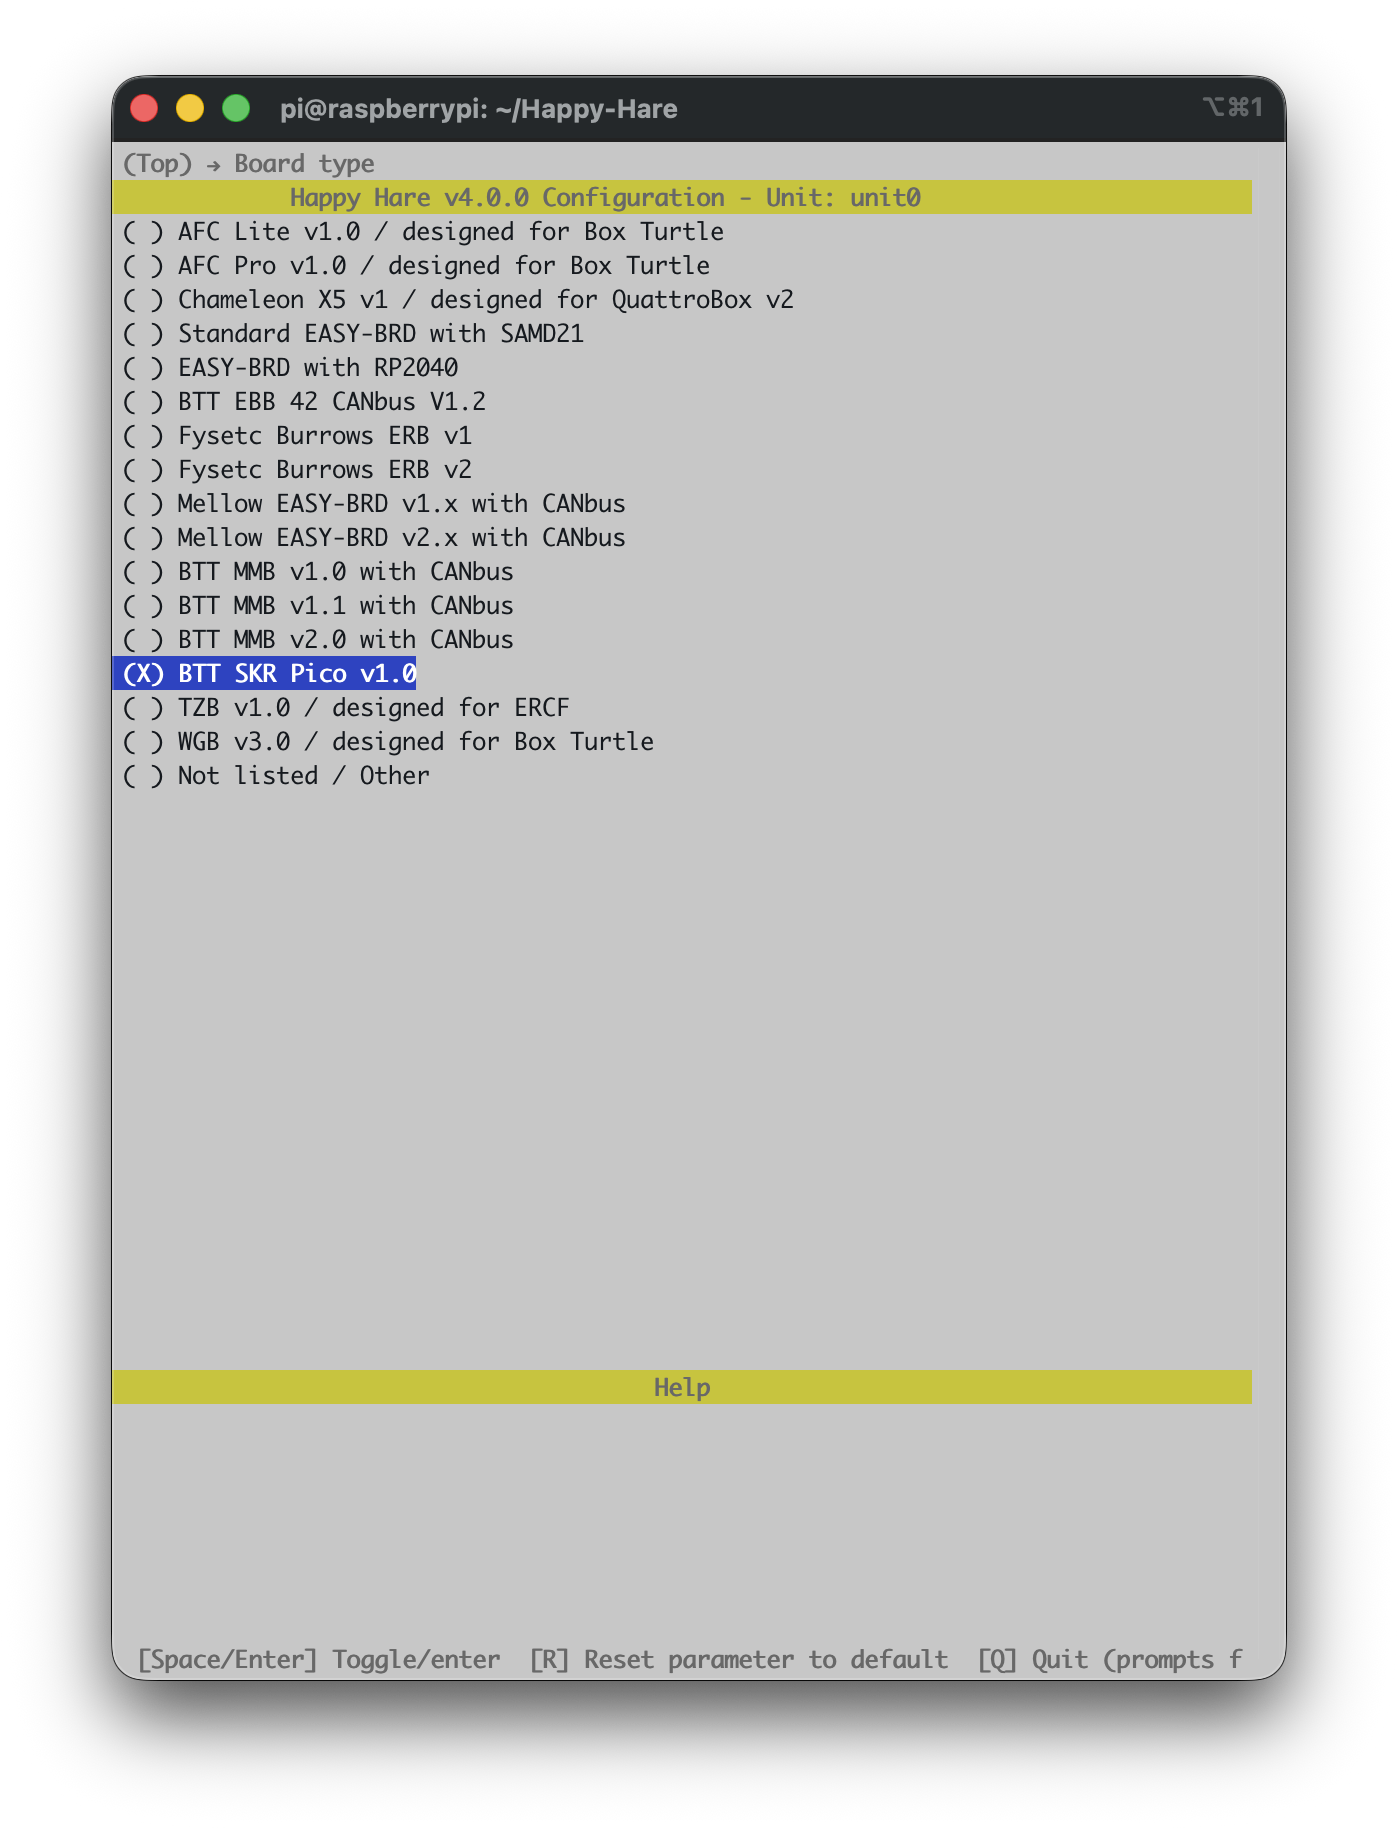
Because you already told it this is a 3MS, Happy Hare has pre-selected BTT SKR Pico v1.0 — the board most 3MS builds use. If your build uses a different controller board, this is where you'd pick it instead; the pin defaults for every stepper, sensor and TMC driver on the rest of the menu come from whatever you choose here.
MCU connection
Back out to the top and enter MCU connection:
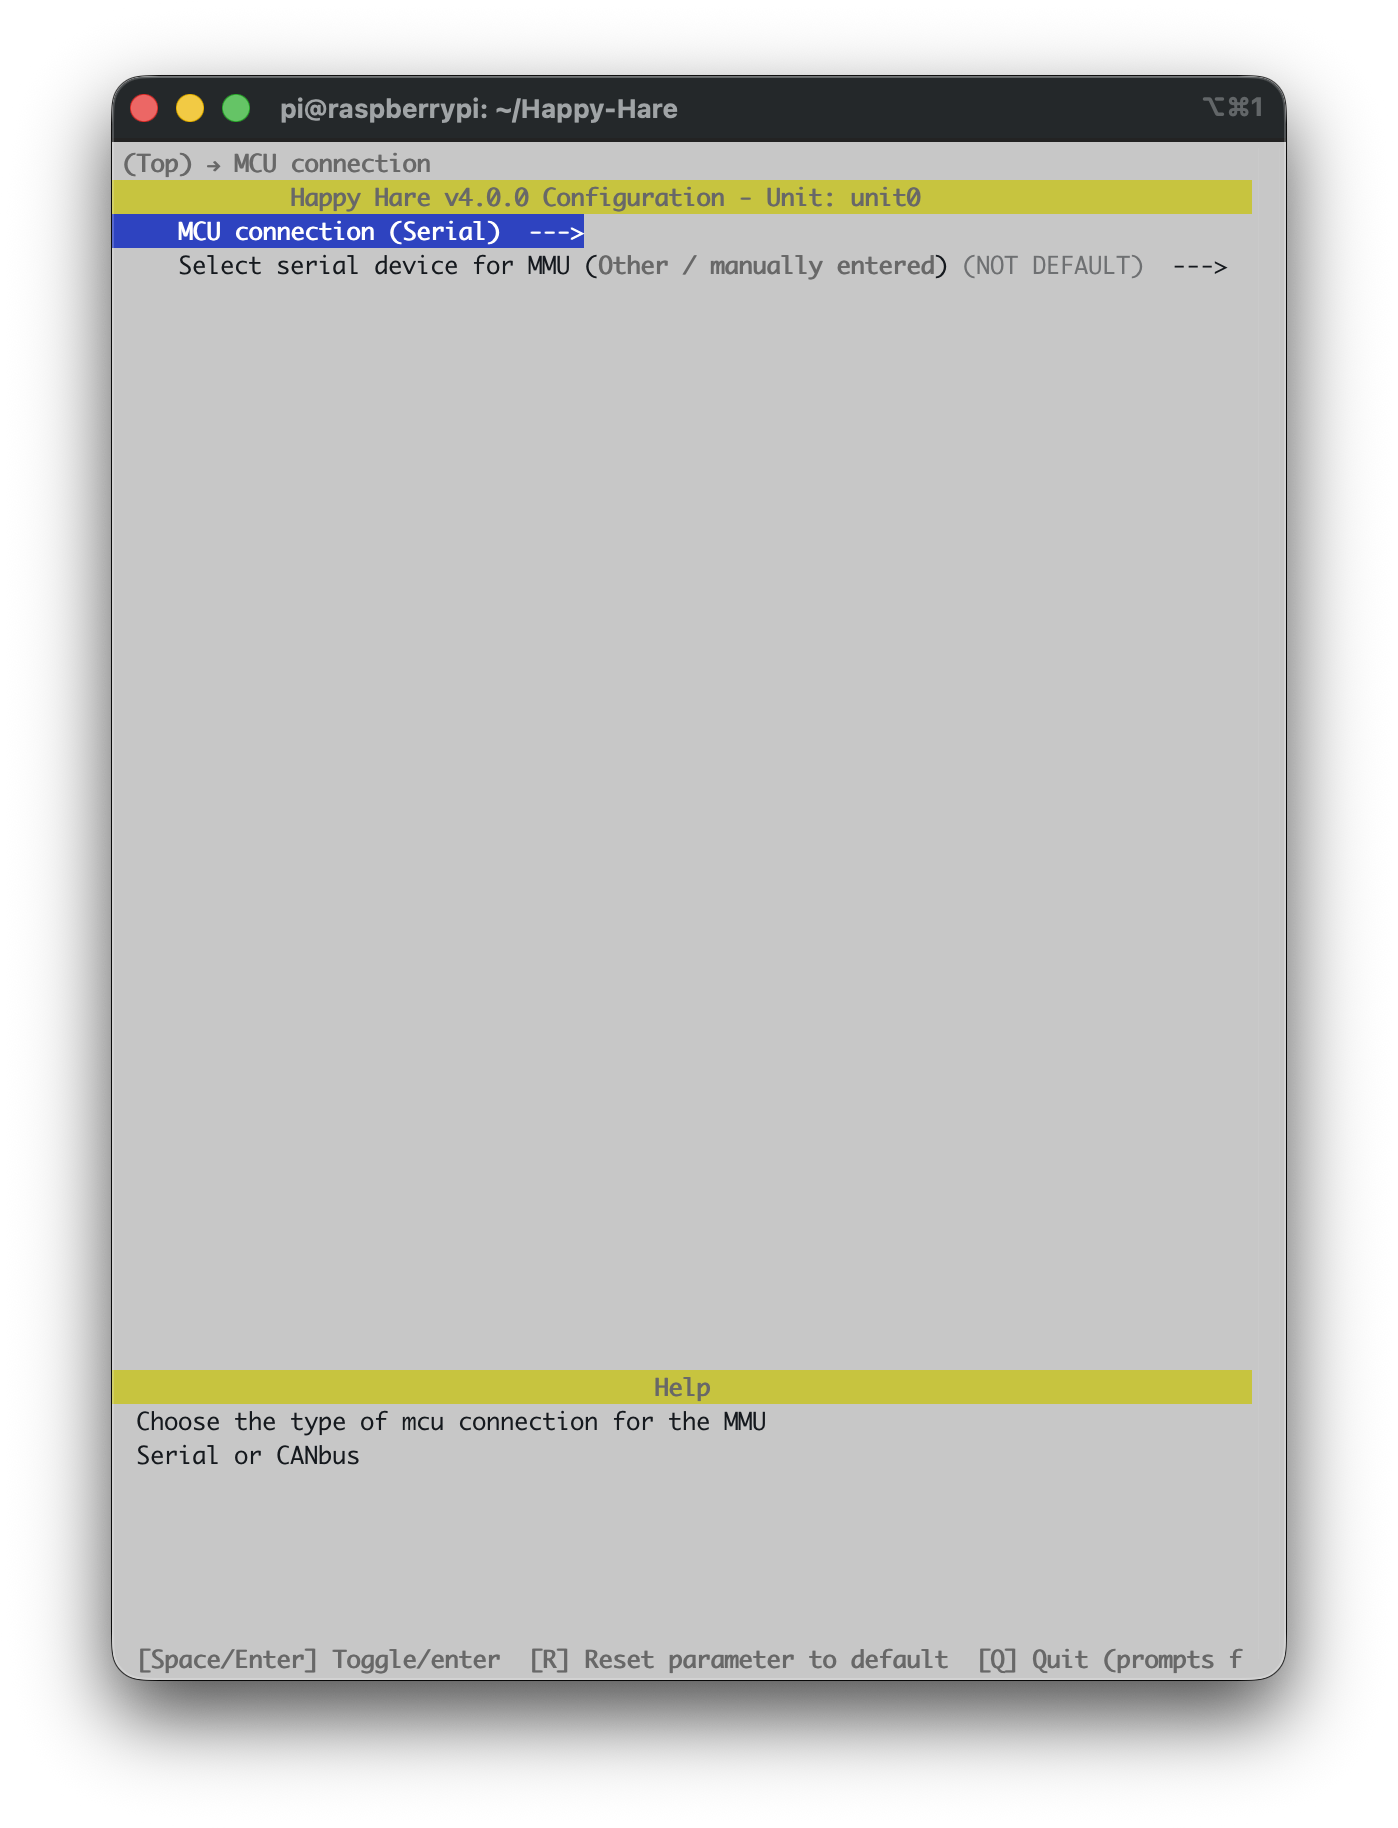
Again, already right for a board like the SKR Pico that plugs in over USB:
MCU connection is Serial, and there's a second line to pick which serial
device if you have more than one board attached. If your board talks CANbus
instead, this is where you'd switch it — but for a stock, USB-attached 3MS, Serial is what you want and there's nothing to change.
MMU Features / Additions
Back out and enter MMU Features / Additions:
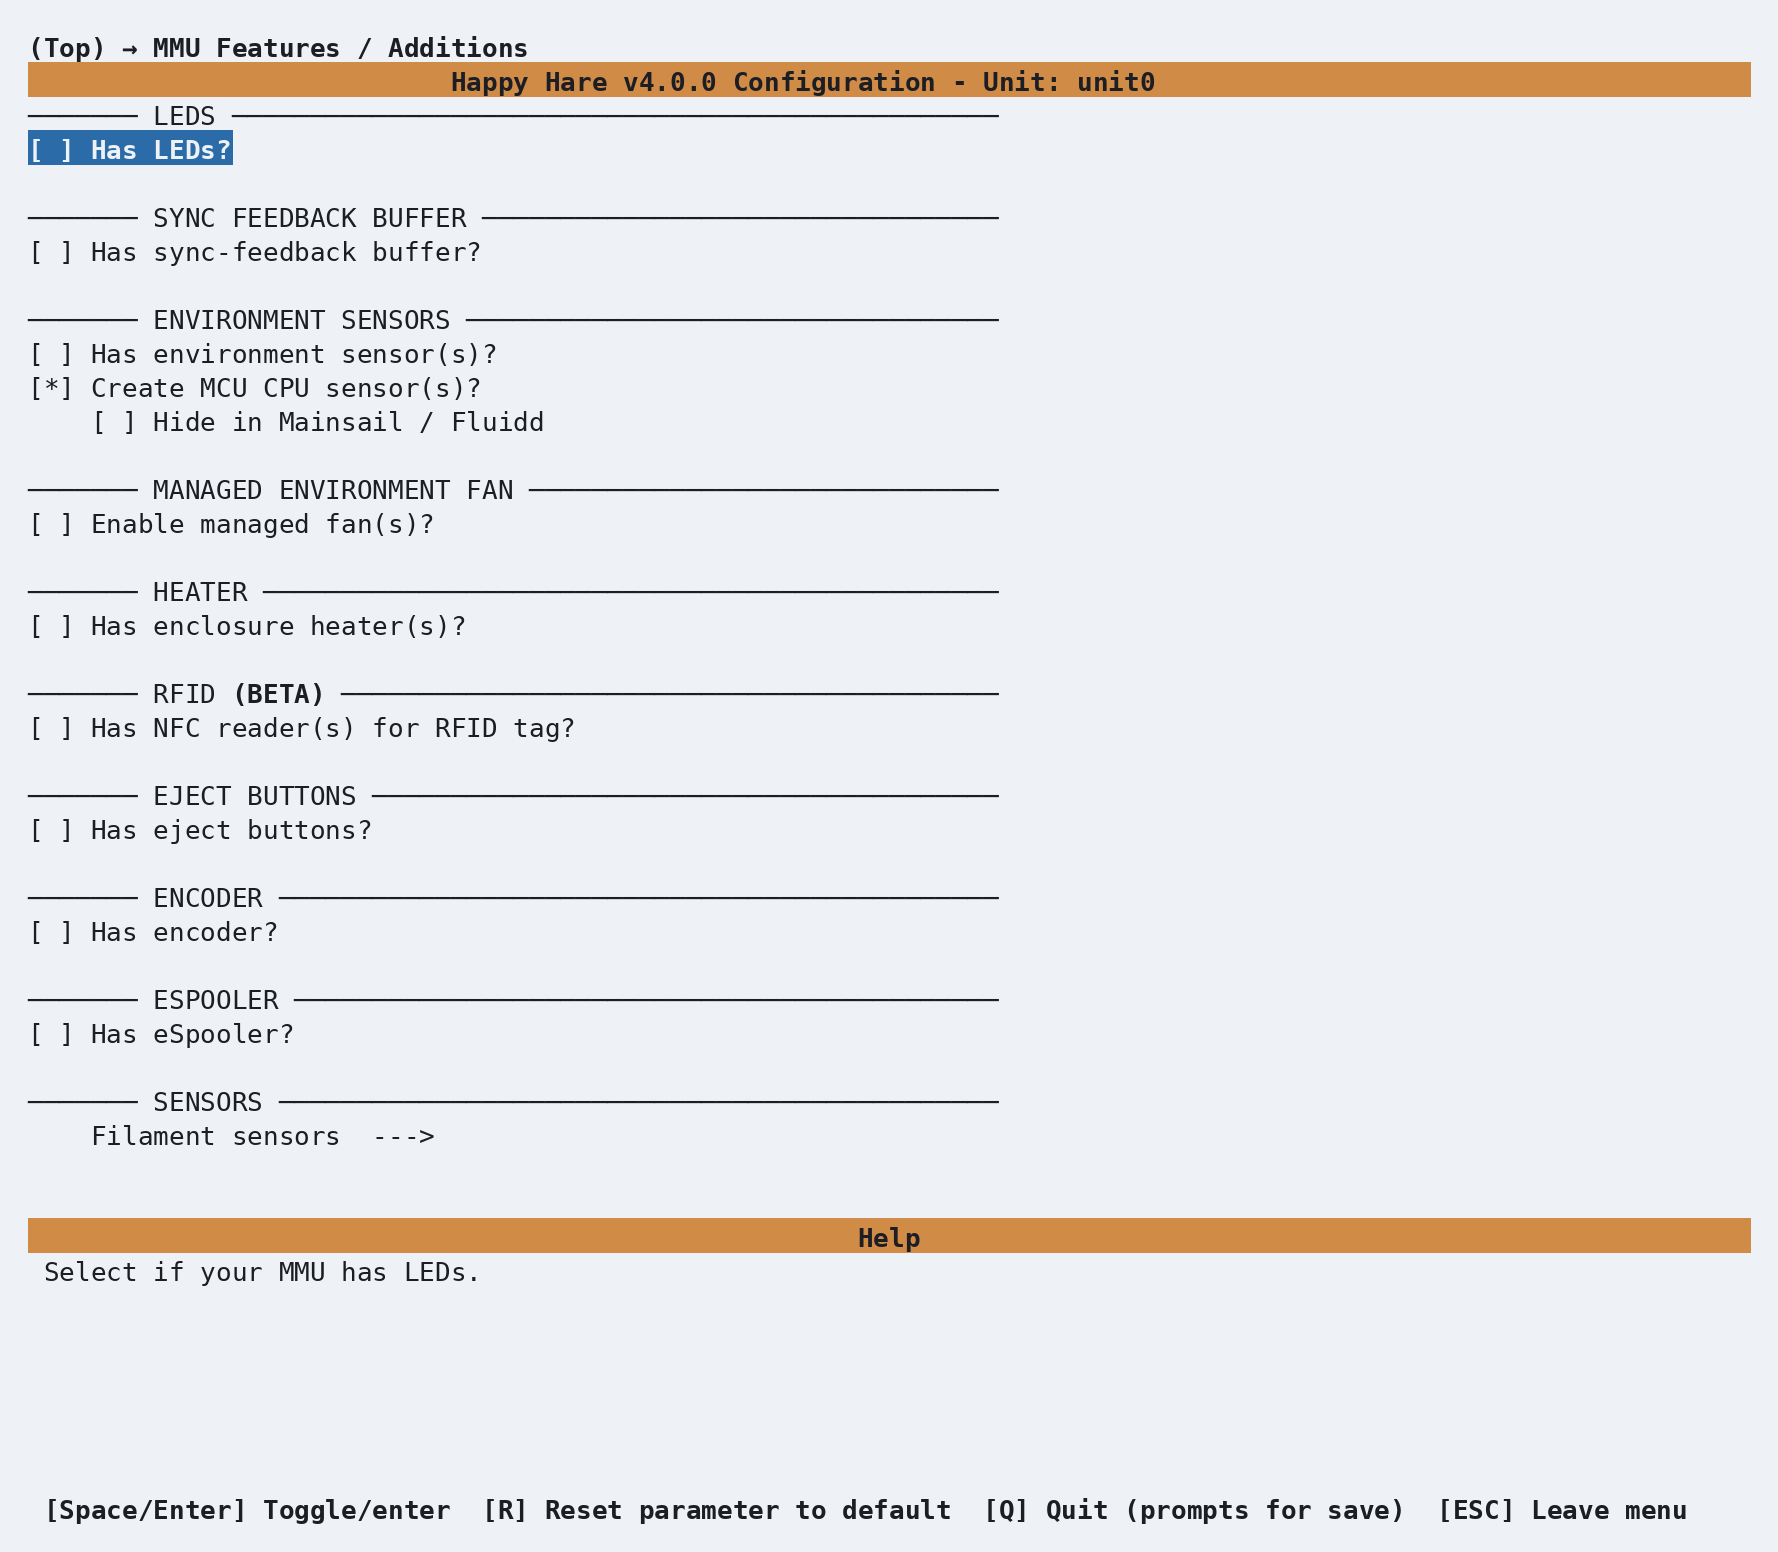
This is worth a look even though — for a stock 3MS — there's nothing to add. The MCU temperature sensor is already switched on. That makes the managed-fan option available, but it remains off until you enable it; only do so when a fan output is actually wired. Since the 3MS is an open-ended design, you can also add an environment sensor, heater or any other feature present in your build. If you're following this page for a plain, stock 3MS, just look and move on.
Pins: gear direction
Back out to the top, enter Pins / TMC, then Gear pins:
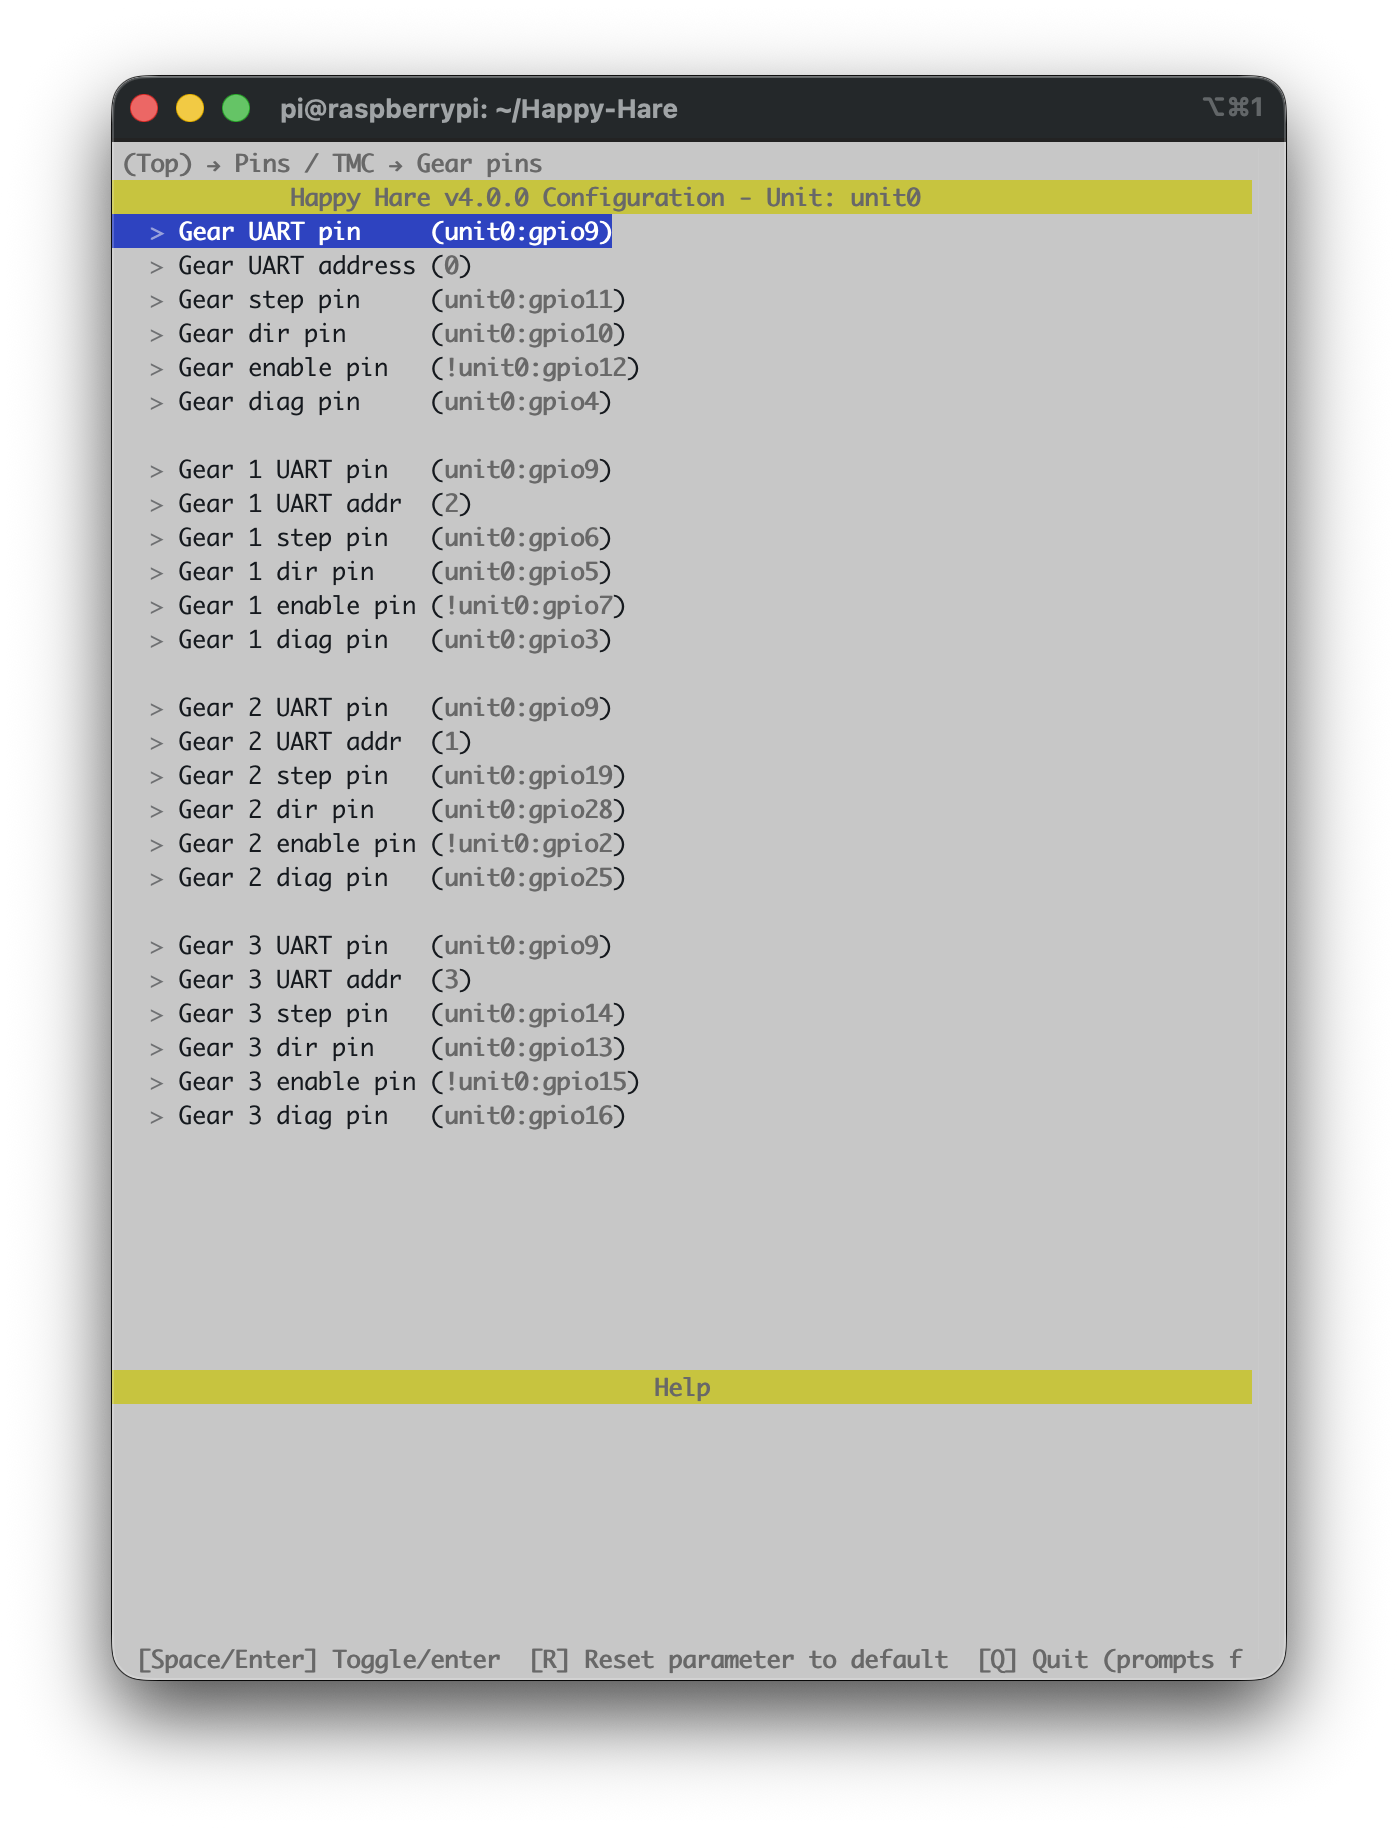
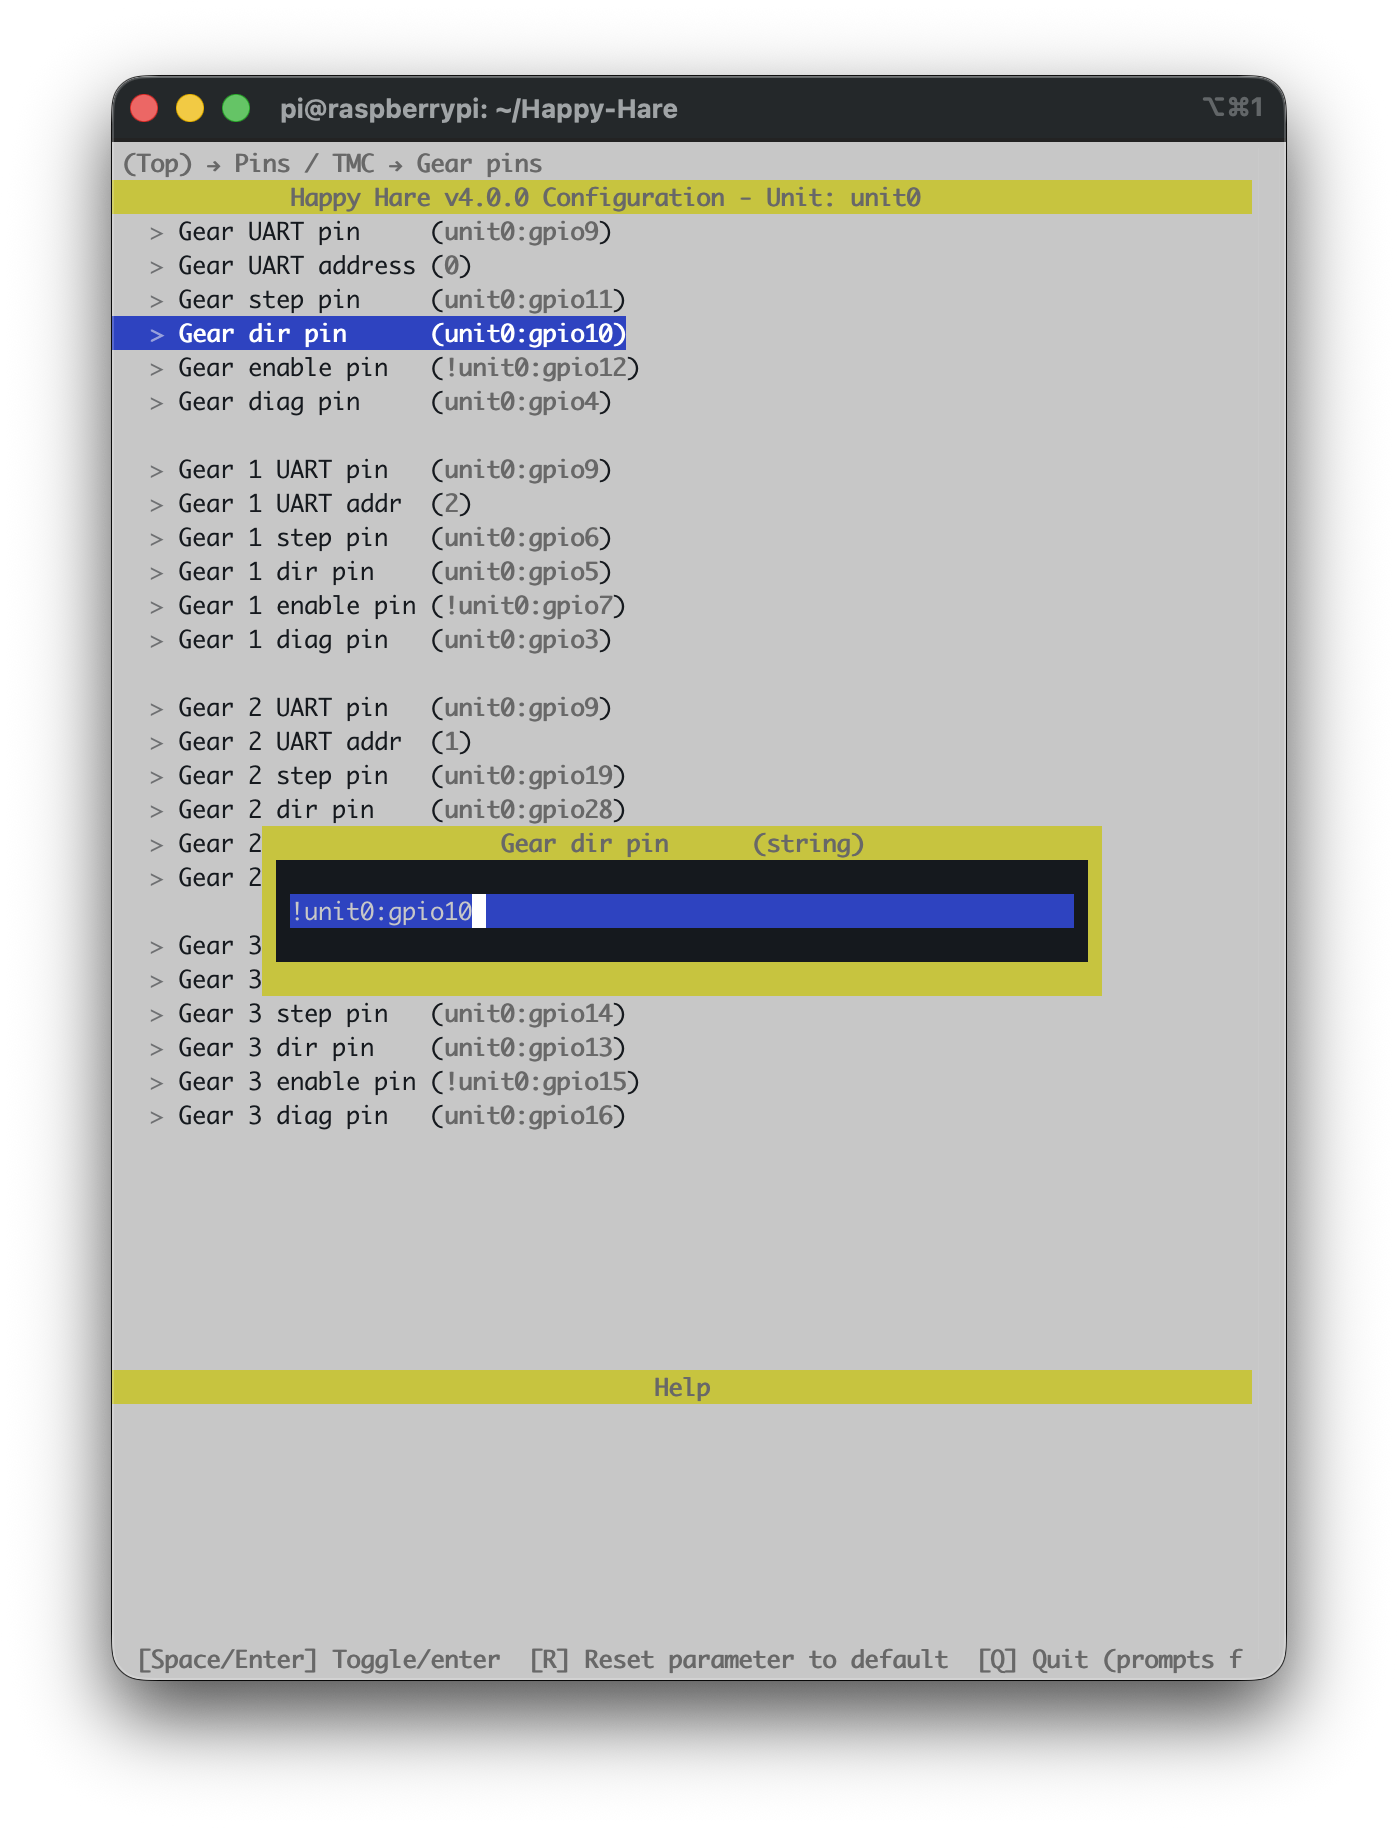
Every gate has its own UART, step, dir, enable and diag pin, all filled in from the SKR Pico defaults you picked earlier. The one you're most likely to need to touch is dir — whether a gear stepper spins the "right" way depends on which way its cable happens to be plugged in, and no config file can know that in advance. You'll find out the first time you try to load filament and gate 0 (say) runs backwards.
Highlight Gear dir pin and press Enter to open its editor:
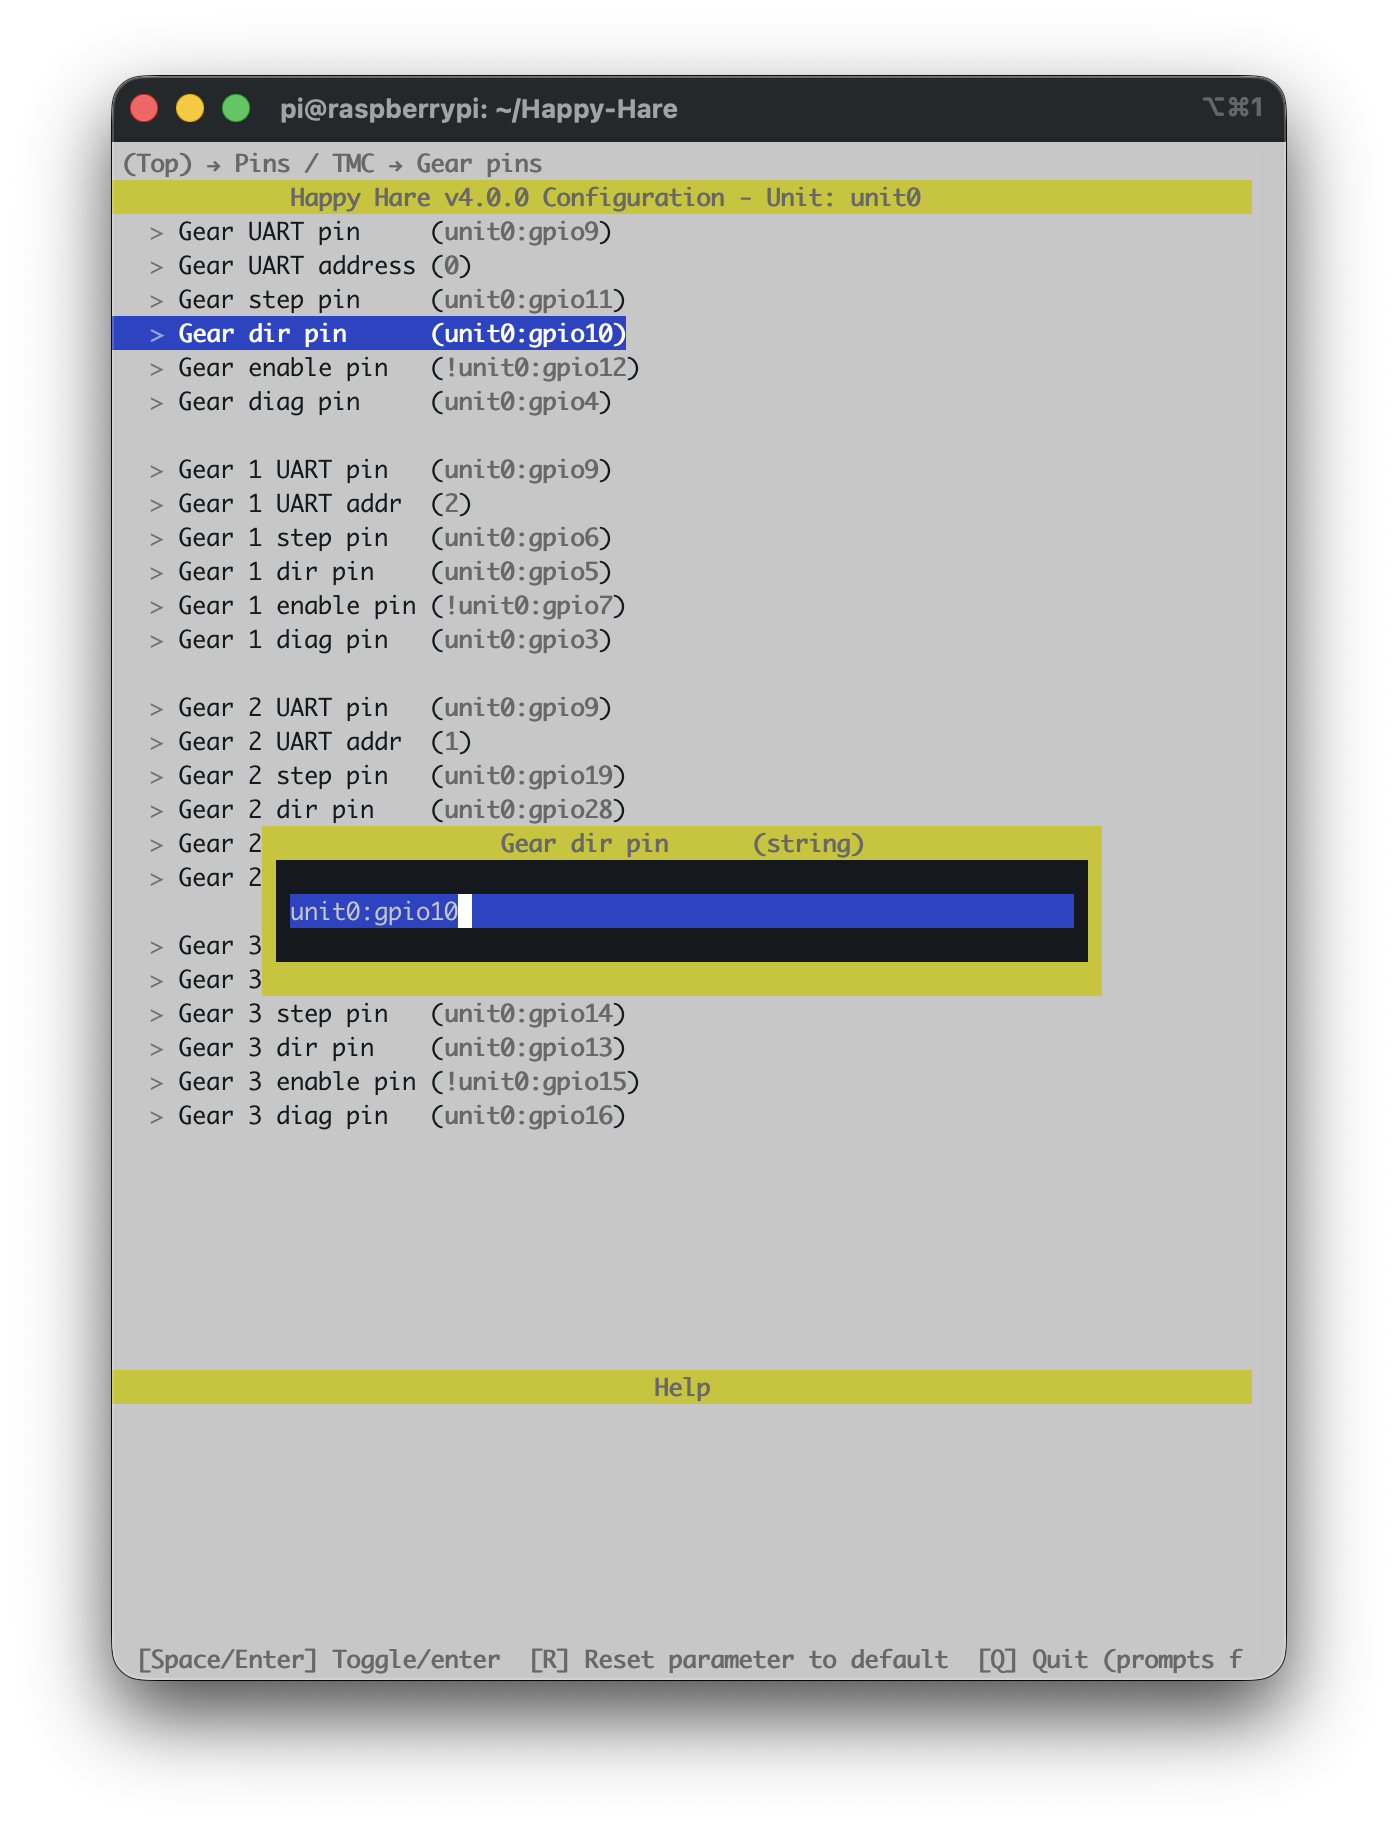
If that gear needs reversing, add a ! in front of the pin name — Klipper's
standard way of inverting a pin's polarity:
Tip
If you built your 3MS from a kit, enter each of the dir pin entries and add a "!" in front of the pin to invert it.
That's it — no rewiring, no .cfg files to hand-edit. Press Enter to accept the
change, or Esc to back out without applying it. And if you ever change a value
here and decide you'd rather have the default back, that's exactly what the R
key mentioned earlier is for: highlight the parameter and press R, and it resets
to whatever Happy Hare would have picked on its own.
Picking a toolhead
From the top menu, enter Toolhead:
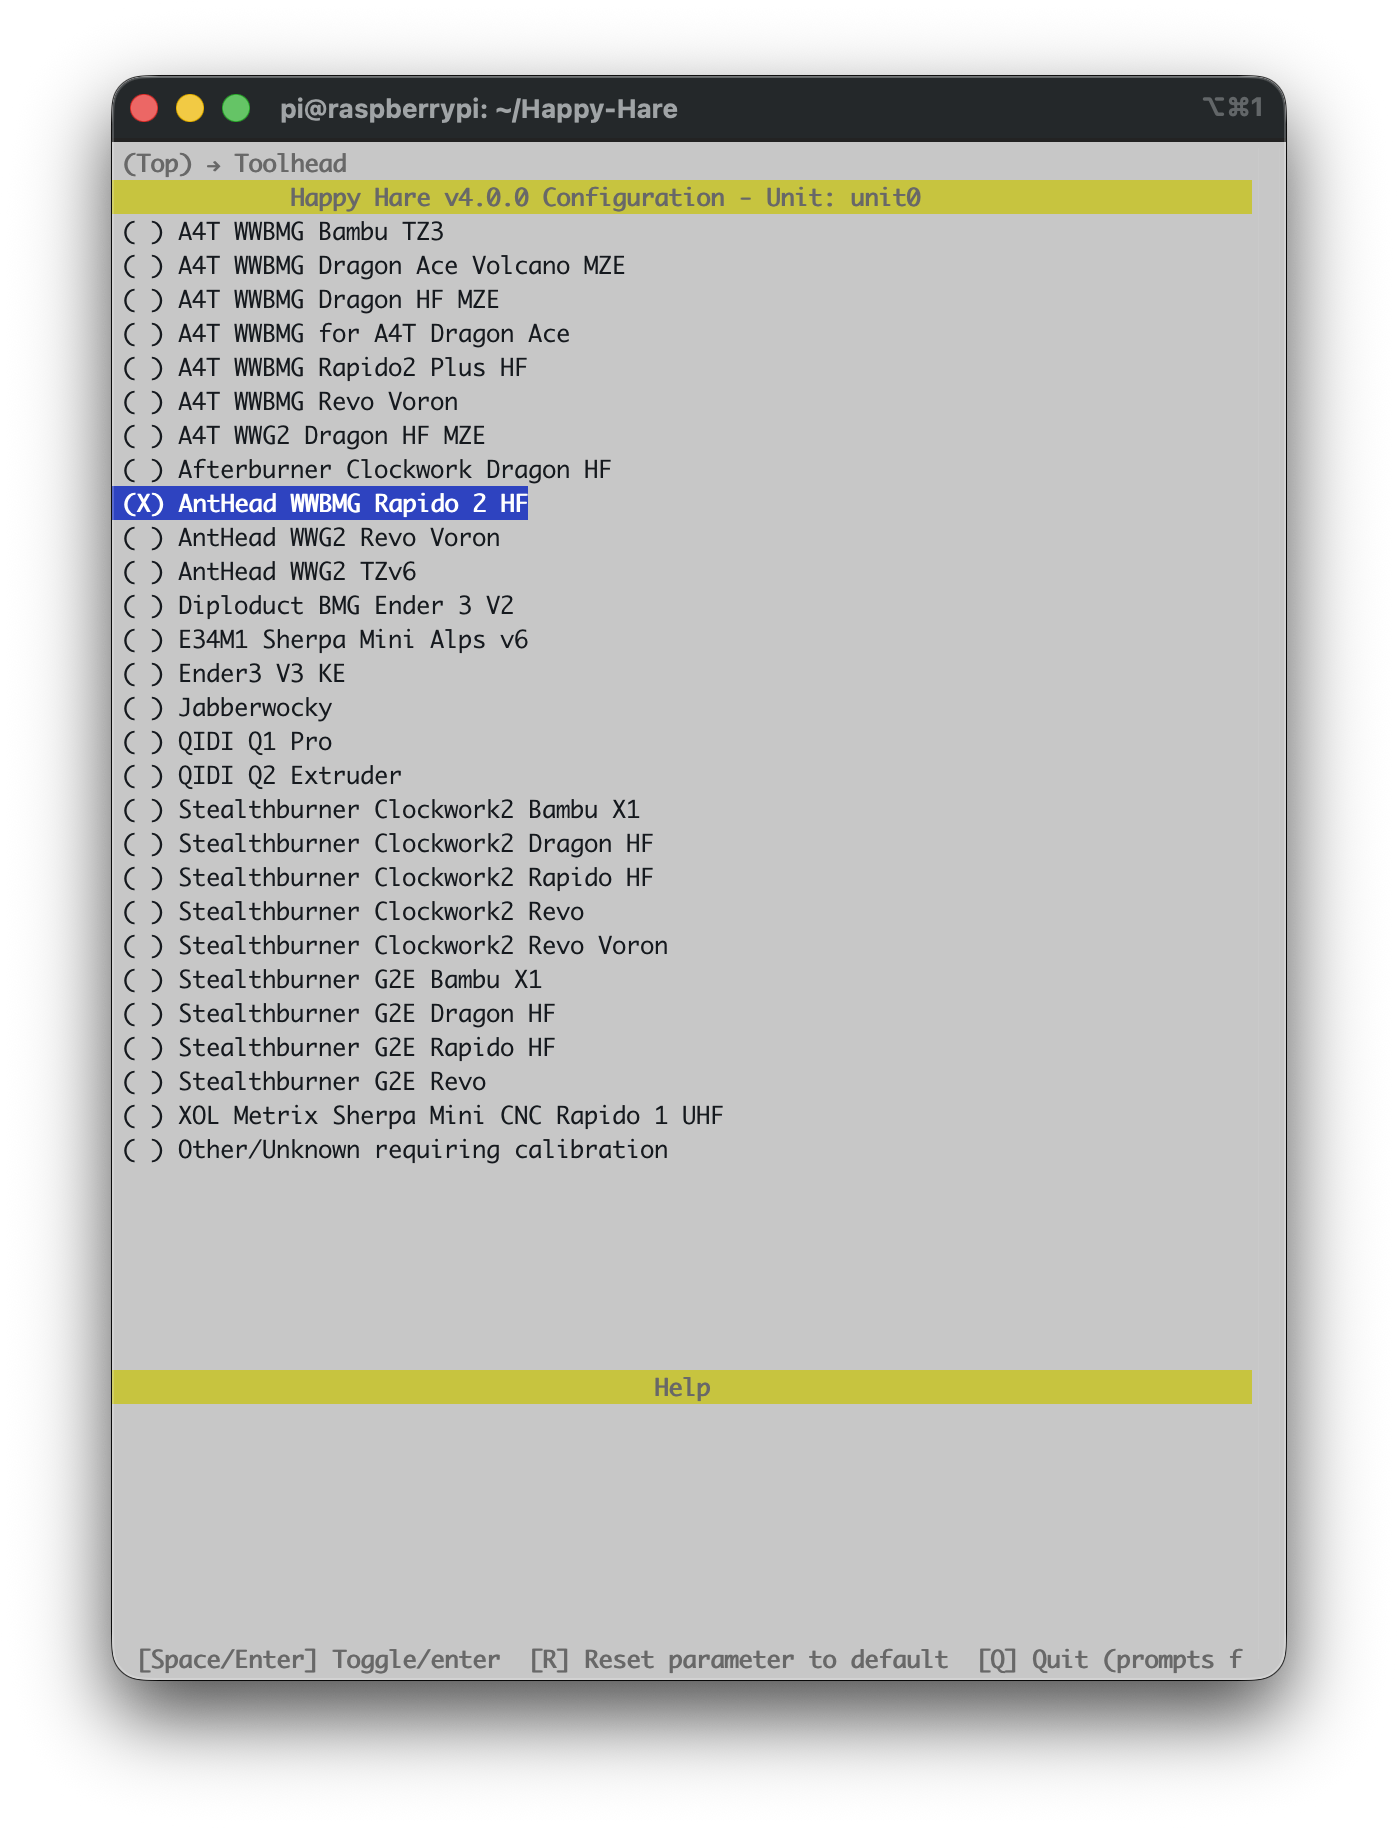
This step is entirely optional — skip it and Happy Hare falls back to generic "Other/Unknown" dimensions, which is a perfectly normal starting point. But if your toolhead (extruder + hotend combo) happens to be in this list, picking it gets you real, community-measured values instead of guesses, for free. Here we've picked AntHead WWBMG Rapido 2 HF at random, just to show what selecting one does.
Back out and enter Toolhead sensors/settings to see the effect:
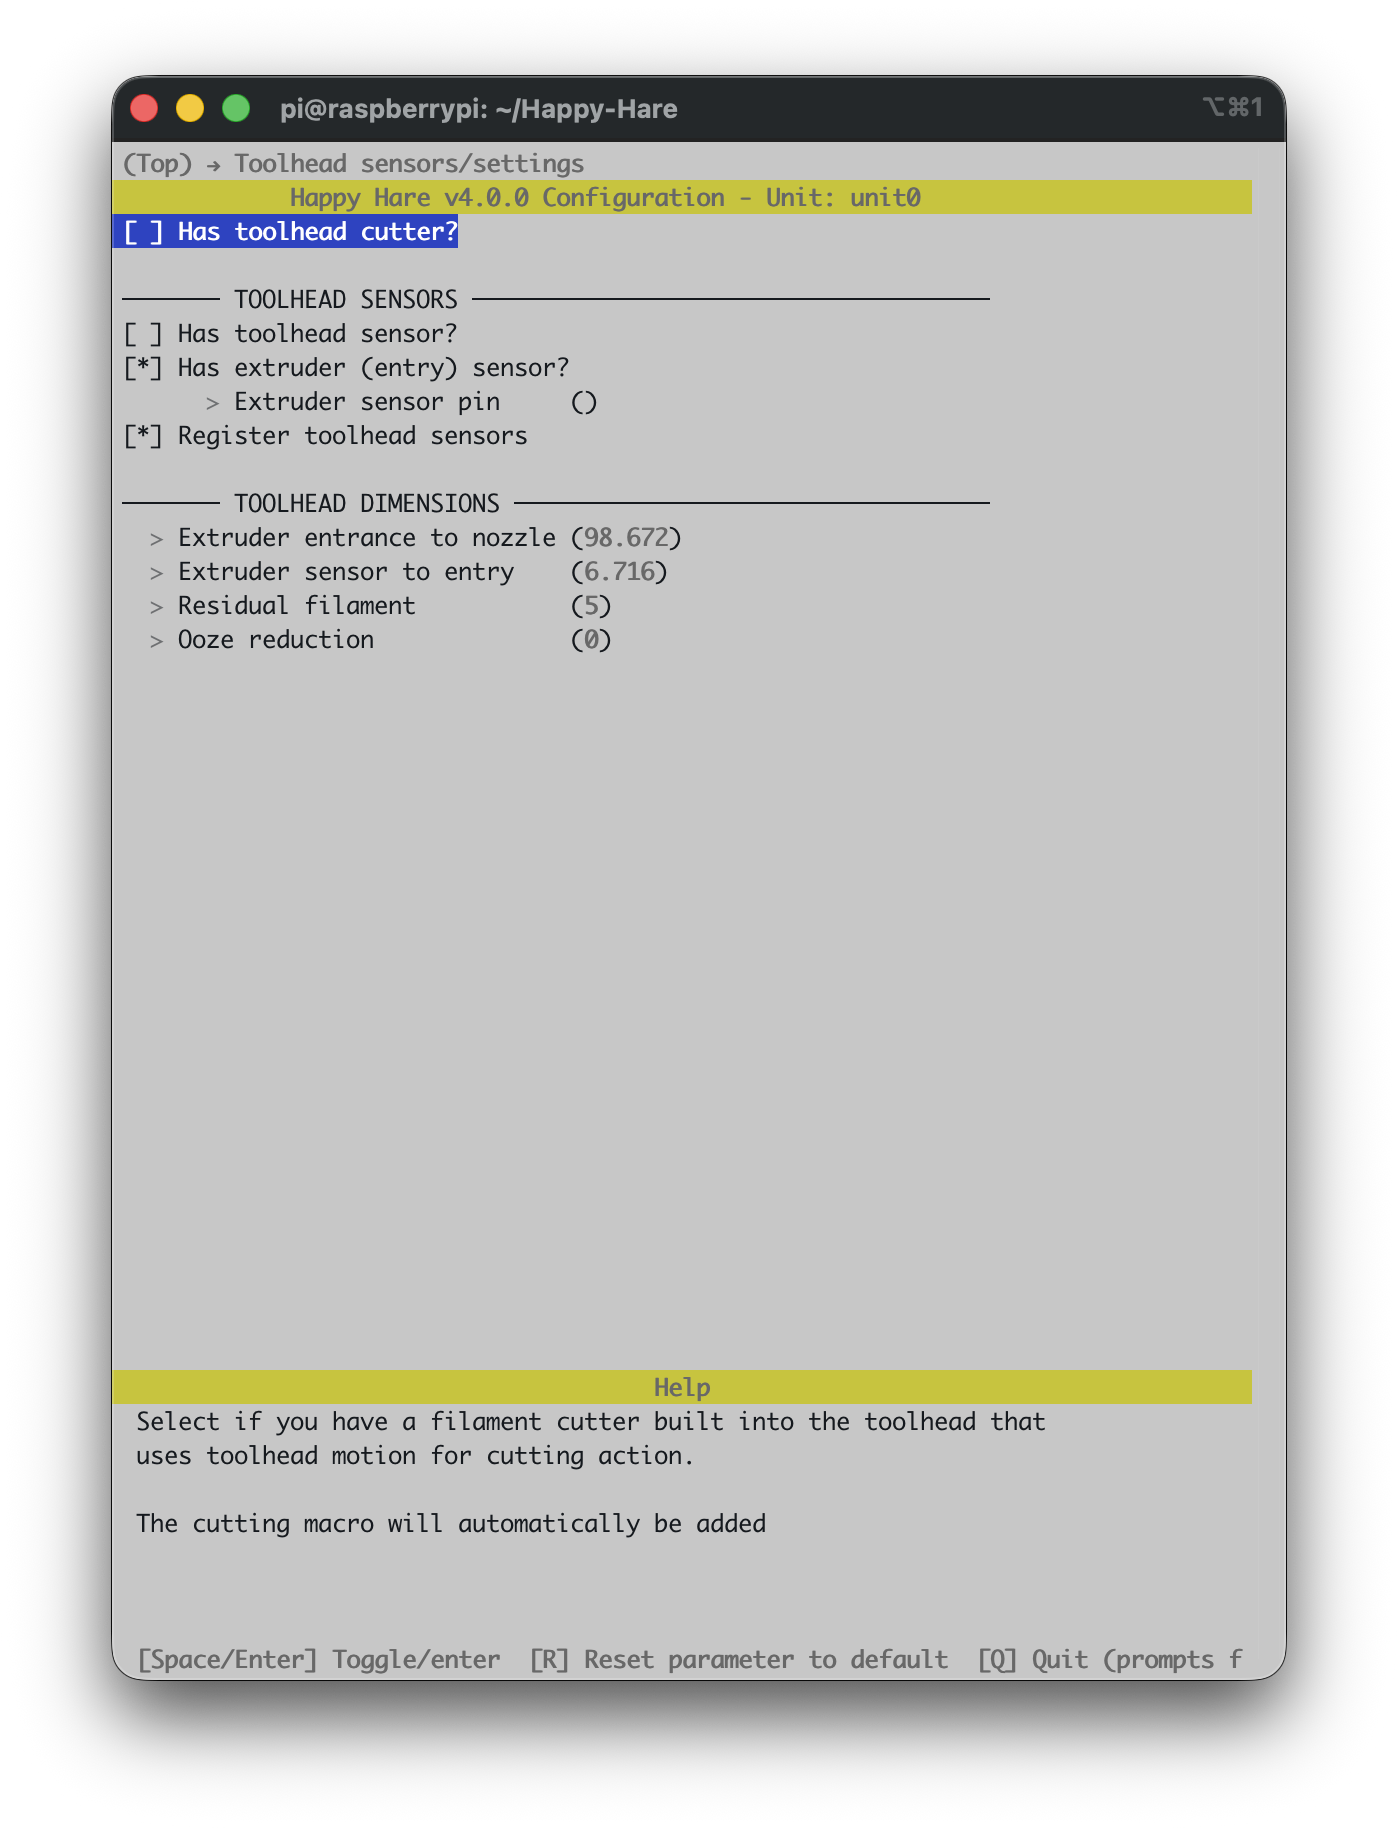
Extruder entrance to nozzle and Residual filament, under Toolhead dimensions,
are already filled in — 98.7 and 5 here — measured by someone else on the same
hardware rather than left at the generic default. The other two distances Happy Hare
can use (toolhead sensor to nozzle, extruder sensor to entry) only appear once you've
told it you actually have those sensors on your toolhead, higher up this same screen --
until relevant the values stay hidden here.
Contributions to the toolhead list are always welcome! If you would like to contribute your parameters to this toolhead database, please visit here to add your parameters to future installer updates.
This is a shortcut, not a substitute: even with a listed toolhead, you're still
better off learning to measure and calibrate your own eventually, since small
build variations and mods add up. But it's a genuinely good starting point,
and if your exact combo isn't listed, "Other/Unknown" plus manual calibration
(MMU_CALIBRATE_TOOLHEAD) is exactly as normal a path as this one.
An example software option: Spoolman
From the top menu, enter Software Options, then Select spoolman spool manager support:
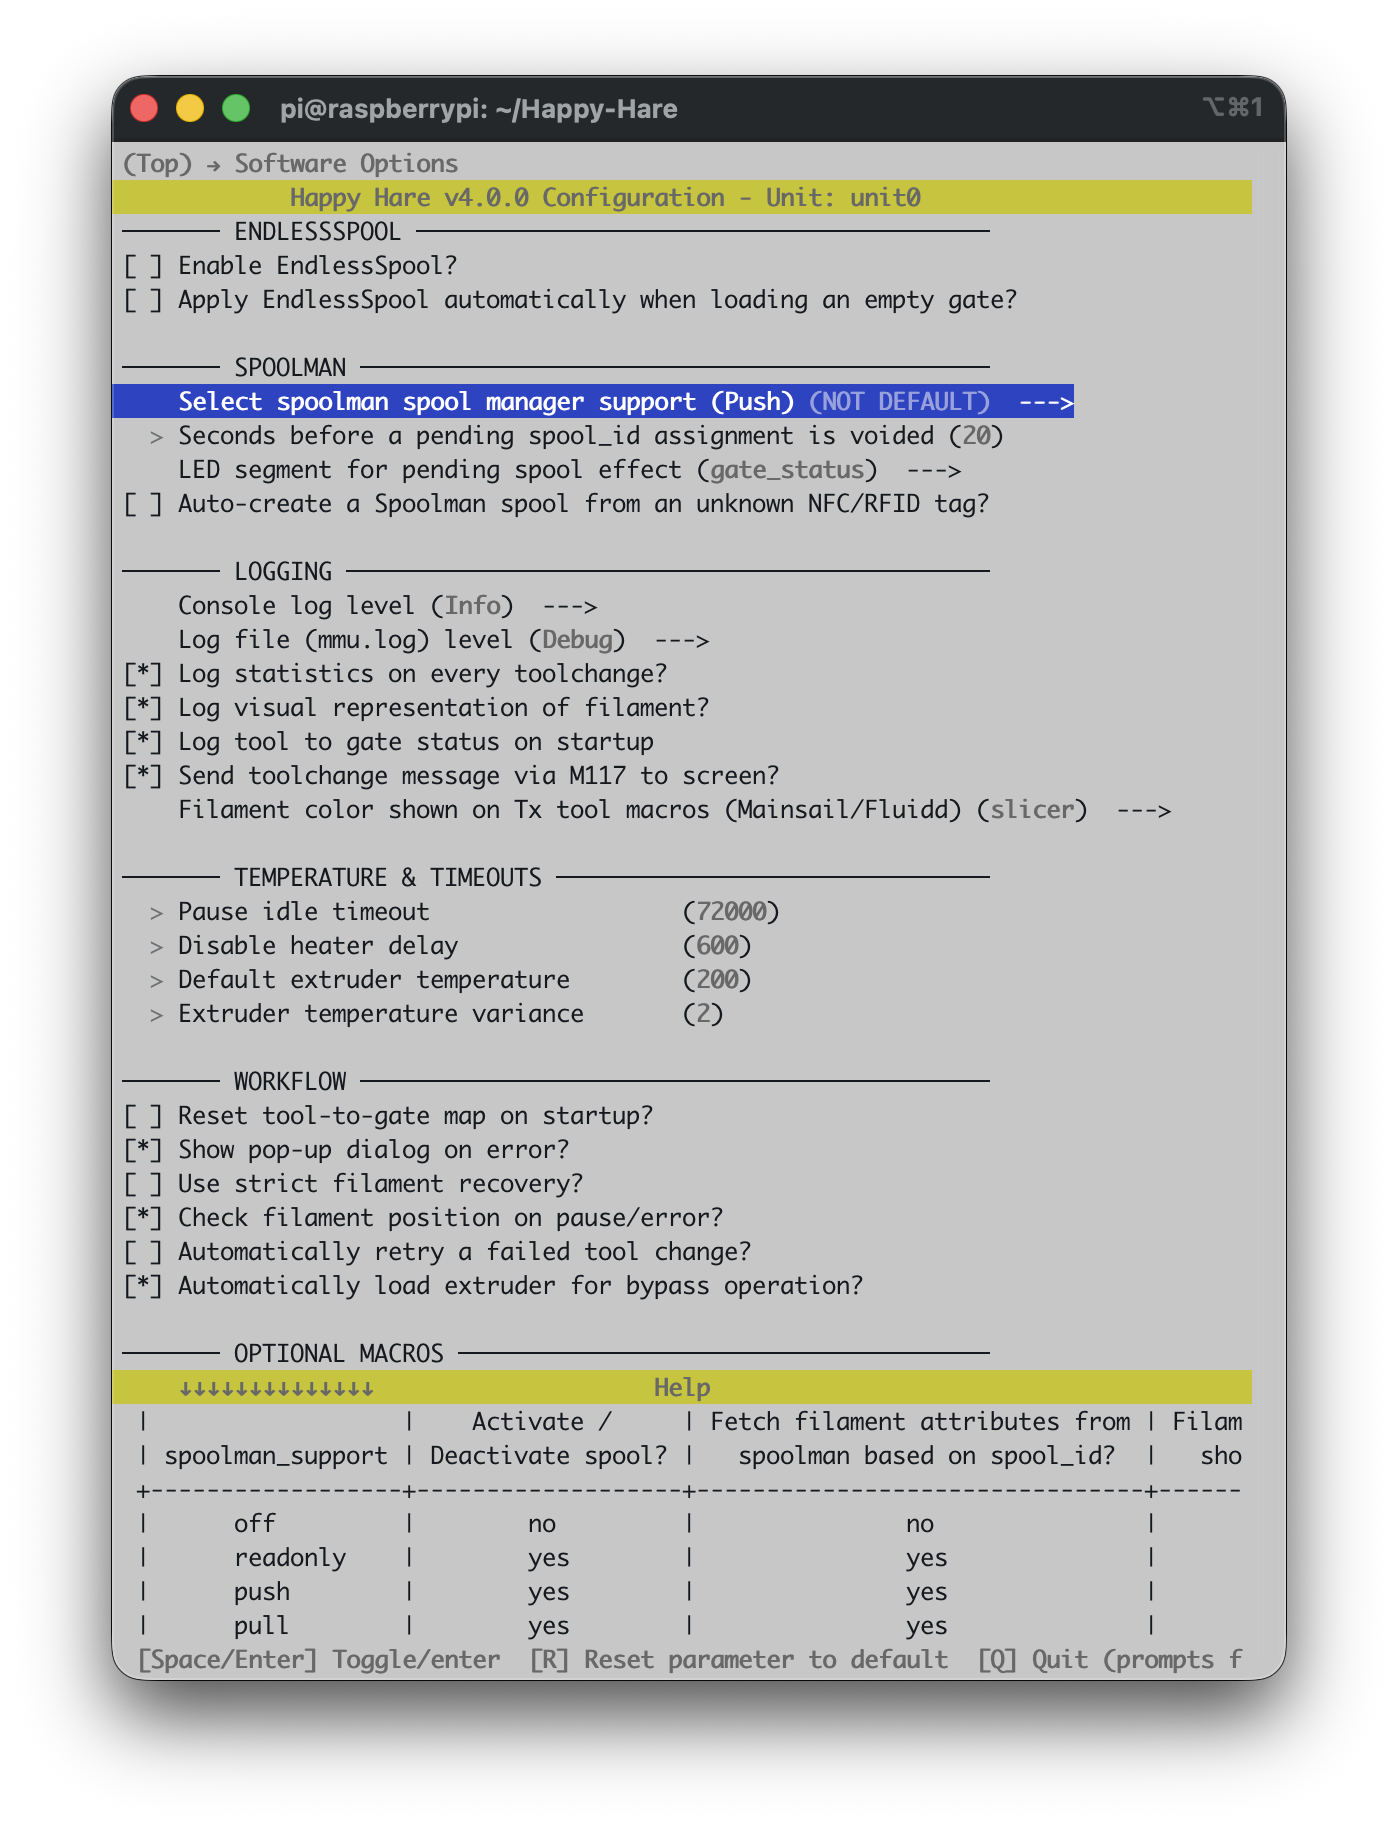
This is one small example of the many software-side options living under Software Options — most of them, like this one, default to off and are entirely optional. If you run a Spoolman instance and want Happy Hare to control filament details (material, color, temperatures) for each gate and save them in Spoolman, select Push as shown here. The help table on screen lays out exactly what each of the four modes does — off, read-only, push, and pull — so you can pick the one that matches how you actually use Spoolman.
Notice the row now reads (Push) (NOT DEFAULT) — menuconfig always flags a
value that differs from its default this way, which makes it easy to spot your
own changes later. If you decide you don't want it after all, R puts it straight
back to Off.
Explore the rest
That's enough to get a stock 3MS basically talking to Klipper, but it's
only a fraction of the menu. Software Options, Tip Forming / Cutting,
Purging, Endstops and Bowden movement and the rest are all worth a look —
scroll all the way from the top to Paths & Services at the bottom at least
once. Nothing you look at will break anything: moving the highlight
costs nothing, and R is always there to undo a change you don't
want. Remember that you don't need to setup everything now — you can come back
many times and re-run menuconfig with ./install.sh -i and incrementally
setup features and macros.
Saving, and coming back later
When you're done, press Esc from the top level (or Q) to get the save
prompt, and confirm. Happy Hare writes your .cfg files from what you chose.
The installer only forces menuconfig open automatically on that very first run.
After that, running ./install.sh again just upgrades in place — it won't reopen
the menu. To go back in and change something, use:
./install.sh -i
This is the normal way to revisit any setting on this page — there's no need to
ever hand-edit the generated .cfg files directly.
Note
The one thing worth knowing:
if you've hand-edited a .cfg file since your last visit to menuconfig,
-i will ask how to reconcile that — Refresh (keep your manual edits, and
just add new options), Replace (regenerate everything from menuconfig, discarding
direct edits) or Merge (attempts to merge manual edits into menuconfig)
If you only ever configure through menuconfig, as this page assumes, option 2
(Refresh) is the recommended choice because it rebuilds your Happy Hare
klipper config files ensuring a clean config and any future update made to the
Happy Hare software.
Validating Hardware Setup
With Klipper accepting the config and no startup errors, confirm the physical mechanism actually does what Happy Hare thinks it does before calibrating anything or trying to print.
Gear stepper direction. Each gate has its own gear stepper, and which way it spins depends entirely on how its motor cable happens to be plugged in. Check each one — feed a scrap of filament in by hand first so you can see which way it moves:
MMU_SELECT GATE=0
MMU_TEST_MOVE MOVE=50
It should feed forward, away from the spool. If a gate runs backward,
give that gate's Gear dir pin a ! (see Pins: gear
direction above) and try again. Repeat with
GATE=1, GATE=2, GATE=3.
Sensors. Insert a short fragment of filament into your toolhead's entry sensor by hand and check it registers:
MMU_SENSORS
extruder              --> TRIGGERED
toolhead              --> Open
Remove the fragment and confirm it goes back to Open. Do this for every
sensor you plan to use.
Calibration
See Calibration for the full picture (which steps apply to which MMU type, and why) and Calibration: Gear Rotation Distance for the complete procedure.
Checking Basic Operation
Outside of a print, confirm the basics work end to end on a gate you've already validated above:
MMU_SELECT GATE=0
MMU_LOAD
MMU_UNLOAD
Each should complete without error — no pauses, no "not calibrated" warnings you weren't expecting. If something goes wrong here, it's much easier to diagnose now than mid-print; see Operation: Debugging Problems if any of it doesn't behave as expected.
Slicer Setup
You now need to add some gcode hooks into your favorite slicer for start g-code,
end g-code, after layer change and on tool change. This is to coordinate with
the MMU during certain phases of a print. This is covered in
Slicer Setup. Jump to this section, make these
changes and return here.
Printing with MMU
Besides the slicer gcode hooks above, there's one real decision left before your first multi-material print: how purging between colors happens.
- Slicer-controlled — your slicer's own wipe tower, printed alongside the model. Simplest to set up; costs bed space and filament.
- Happy Hare-controlled — a dedicated purge macro runs at each toolchange instead of a wipe tower: either Macro: Purge (simple, prints a purge line) or Macro: Blobifier (a dedicated purge/park station, more capable but its own hardware). See Purging without a wipe tower for how to disable the slicer's tower and hand purging over to Happy Hare.
Either way, the toolchange parking positions and movement (retraction,
z-hop, where the toolhead parks during a change) live in
mmu_macro_vars.cfg, tunable through Macro Variables in menuconfig
— see Toolchange Movement for what each setting
actually does before changing the defaults.
Once that's decided, slice something with more than one filament and run your first print.
What Next?
- Install KlipperScreen (Happy Hare edition) if you want a touchscreen front end, or drive everything from Mainsail / Fluidd — either works, and both are covered.
- From here, explore the rest of this site's Features section one page at a time as you actually need them — Spoolman integration, NFC/RFID tags, EndlessSpool, and the rest. Trying to absorb all of it before your first print is the fastest way to feel overwhelmed by an MMU that, day to day, mostly just works.